7 CNC Precision Machining Tips for Global Buyers
Buying CNC Precision Machining services across borders involves more than comparing hourly rates. A low quotation can hide weak inspection systems, unclear tolerances, or costly rework. Experienced buyers examine drawings, materials, surface finishes, production capacity, and quality records before approving a supplier. They also ask how measurements are recorded, not merely whether inspection exists.
Shigeo Shingo, a respected manufacturing engineering expert, said, “The most dangerous kind of waste is the waste we do not recognize.” This principle applies directly to international machining projects. Unnoticed waste may appear as excessive scrap, repeated engineering questions, poor packaging, or delays caused by incomplete specifications. Small details matter.
This guide presents seven practical CNC Precision Machining tips for global buyers. It considers supplier verification, material certification, tolerance control, sampling, communication, logistics, and total cost. A capable manufacturer should explain its process clearly, from tool selection to final inspection. Look for calibrated equipment, documented procedures, and evidence from comparable projects.
Still, no sourcing method is flawless. Even careful buyers can overlook a critical datum or misread a tolerance note. We have seen minor drawing assumptions create major production problems. That is why technical reviews should involve both purchasing and engineering teams. Clear questions reduce uncertainty before metal reaches the machine.
The following recommendations are designed for real purchasing decisions. They help buyers compare suppliers fairly, manage technical risk, and build dependable long-term partnerships.
Define Precision Machining Requirements Before Requesting Quotes
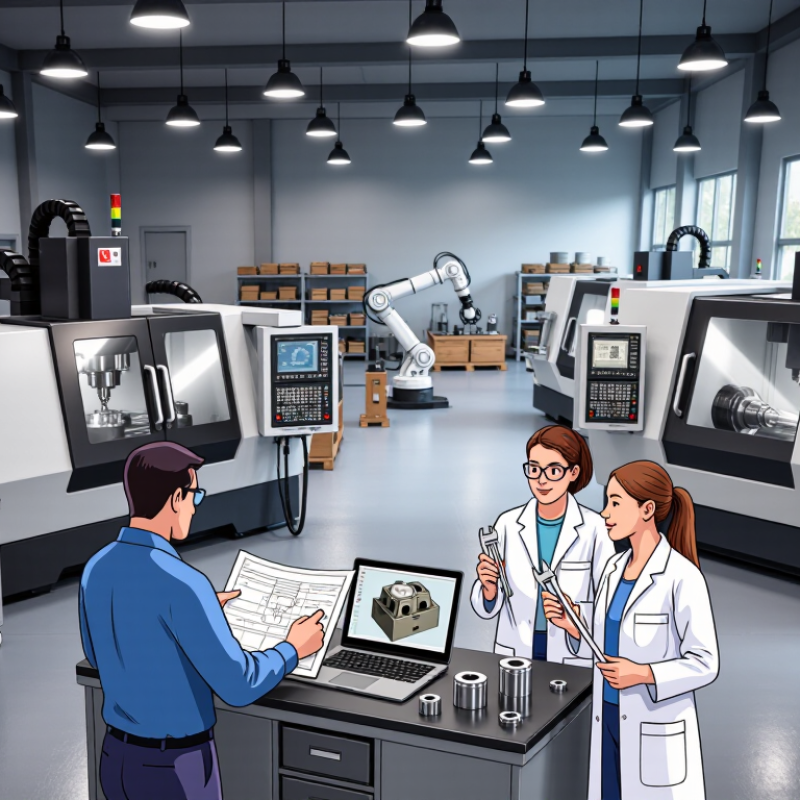
A precise quote begins with a precise requirement. Describe material grade, part quantity, annual demand, and delivery location. State critical dimensions, tolerance zones, surface roughness, and thread standards. A drawing alone may not explain functional priorities. It can still be incomplete.
The 2023 ISO Survey reported 1,265,216 ISO 9001 certificates across 189 countries and economies. This figure shows the importance of controlled quality systems, but certification alone cannot prove machining capability. Ask suppliers for sample inspection reports, calibration records, process capability data, and traceability methods. Specify whether inspection requires CMM measurement, first-article inspection, or a defined sampling plan. Keep it measurable.
NIST guidance on dimensional measurement stresses uncertainty and traceability. Therefore, request the measurement method, equipment accuracy, and acceptance standard before comparing prices. A ±0.01 mm tolerance may require different processes than a general ±0.10 mm tolerance. Confirm datum references, geometric tolerances, deburring limits, and packaging protection. Small omissions create large cost differences.
I have seen buyers request “high precision” without defining precision. That phrase is not enough. Also, the tightest tolerance is not always necessary. Review each critical feature against its real function, then separate must-have requirements from preferences. This step may feel slow. It usually prevents expensive rework.
Select CNC Materials, Tolerances, and Surface Finishes
For global CNC buyers, material selection should begin with service conditions, not a familiar alloy name. Ask about load, temperature, corrosion, weight, and electrical needs. Aluminum suits lightweight housings, while stainless steel supports wet or demanding environments. Engineering plastics can reduce friction, but they may creep under constant pressure. I have seen a small material shortcut create oversized mating parts later. That mistake was avoidable. Request the material grade, heat-treatment condition, and traceability documents before production.
Tolerances should match function. A ±0.01 mm callout across every feature can raise costs without improving assembly. Define tighter limits only for bearing seats, sealing surfaces, or alignment holes. Use datum references and identify critical dimensions clearly. A capable supplier should review the drawing and flag conflicting requirements. Do not assume a nominal CAD size guarantees a perfect fit. Temperature, tool wear, and measurement methods affect results. Some drawings still leave these details vague. That needs correction.
Surface finish changes friction, appearance, and corrosion resistance. Machined surfaces may show visible tool paths, especially on broad faces. Specify roughness values for functional areas and describe cosmetic expectations separately. Anodizing, passivation, plating, or bead blasting can alter dimensions. Allow for that change before final sizing. Ask for sample parts or inspection photos when appearance matters. An inspection plan should state gauges, sampling frequency, and acceptance criteria. It may feel excessive. It prevents expensive surprises across borders.
Evaluate Global Suppliers Through Quality and Capability Checks
7 CNC Precision Machining Tips for Global Buyers
Evaluate a supplier beyond its website and hourly rate. Request sample drawings, material certificates, tolerance plans, and machine lists. Confirm whether its equipment matches your geometry, surface finish, and production volume. A five-axis machine may impress, but it cannot replace proven process control. Ask for recent first-article reports and dimensional records. Check calibration dates for CMMs, micrometers, and gauges. Small details matter.
The ISO Survey 2022 recorded more than 1.26 million ISO 9001 certificates worldwide. Certification shows a quality system exists, not that every part will pass. Review nonconformance records, corrective actions, and traceability practices. Ask how operators control tool wear during long runs. Request capability data, such as Cpk results, for critical dimensions. A supplier should explain the sampling plan in plain language. Vague answers deserve a second look.
Lead-time promises also need evidence. Compare quoted capacity with current orders, maintenance schedules, and subcontracting exposure. Verify packaging, labeling, export documents, and inspection responsibilities before approval. Hold a video audit when travel is impractical. Walk through the raw-material rack, machining area, inspection room, and finished-goods zone. The inspection room should feel organized, not theatrical. A polished spreadsheet can still lie. One weakness is easy to miss: communication quality. Test response times with a technical question, then record how clearly the supplier handles an error. Reflection is necessary; even a careful audit cannot predict every production surprise.
7 CNC Precision Machining Tips for Global Buyers - Evaluate Global Suppliers Through Quality and Capability Checks
| No. | Precision Machining Tip | Supplier Capability Check | Recommended Evidence | Practical Benchmark or Reference | Buyer Decision Signal |
|---|---|---|---|---|---|
| 1 | Match the machine to the part envelope | Confirm the supplier’s CNC mill and turning-center travel, spindle speed, torque, workholding, and maximum workpiece size. | Machine list with model-independent specifications, equipment photographs, sample process sheets, and a review of the largest completed parts. | The machine’s usable travel and chuck or fixture capacity should exceed the finished-part envelope and allow clearance for tools, fixtures, and inspection access. | A strong fit exists when the supplier can explain datum setup, tool access, chip evacuation, and workholding for the actual geometry. |
| 2 | Separate drawing tolerances from process capability | Ask how critical dimensions are controlled and whether the supplier has repeatable data from the same machine, tooling, material, and process. | Capability study, control plan, measurement records, and statistical process control charts for key characteristics. | Cpk ≥ 1.33 is a commonly used production target, but the required value should be agreed according to risk, specification, and customer requirements. | Prefer suppliers that distinguish guaranteed drawing tolerance from typical machine accuracy and support claims with production data. |
| 3 | Verify measurement capability and calibration | Check whether the inspection equipment can measure the required sizes, geometric tolerances, surface characteristics, and form features. | Current calibration certificates, equipment inventory, measurement uncertainty information, and sample inspection reports. | Calibration should be traceable to recognized national or international standards. A common gauge capability expectation is a measurement system variation of 10% or less of total tolerance, subject to the agreed MSA method. | A capable supplier uses suitable CMM, optical, height, roundness, or surface instruments instead of relying only on handheld gauges. |
| 4 | Control material identity and traceability | Confirm that incoming material is identified, segregated, and traceable from purchase through machining, finishing, inspection, and shipment. | Material test certificate, heat or batch number, receiving records, material marking, and chain-of-custody documentation. | EN 10204 Type 3.1 certificates are commonly used for documented inspection results from the material manufacturer; the required certificate type must be specified in the purchase order. | Reject uncontrolled substitutions or certificates that cannot be linked to the actual material batch used for the parts. |
| 5 | Review GD&T, datum strategy, and first-article inspection | Evaluate how the supplier interprets datums, position, profile, runout, perpendicularity, and other geometric requirements before production begins. | Marked-up drawing, manufacturing plan, datum setup diagram, first-article inspection report, and nonconformance records. | ASME Y14.5 and ISO 1101 are recognized references for geometric dimensioning and tolerancing; the governing standard should be stated on the drawing or purchase documentation. | A reliable supplier raises questions about ambiguous datums, inspection direction, bonus tolerance, and measurement fixtures before quoting. |
| 6 | Assess finishing and secondary-process control | Verify control of deburring, heat treatment, plating, anodizing, passivation, coating, marking, cleaning, and packaging. | Approved-process list, subcontractor qualification records, coating or heat-treatment certificates, surface-roughness readings, and final visual criteria. | Surface roughness such as Ra must be measured with a defined method and cutoff length; the drawing requirement, not a generic “standard finish,” controls acceptance. | Prefer a supplier with documented process ownership, defined acceptance samples, and traceability for outsourced operations. |
| 7 | Validate capacity, delivery risk, and change control | Review available machine hours, bottlenecks, preventive maintenance, backup capacity, inspection workload, and the supplier’s process-change controls. | Capacity plan, production schedule, maintenance records, on-time-delivery history, corrective-action reports, and written change-notification procedure. | A realistic lead time should include programming, material purchasing, setup, machining, secondary operations, inspection, packaging, and international logistics—not machining time alone. | Choose suppliers that disclose constraints early, maintain documented revision control, and obtain approval before changing material, tooling, process route, or subcontractor. |
Plan Communication, Packaging, Shipping, and Import Compliance
7 CNC Precision Machining Tips for Global Buyers
Plan Communication, Packaging, Shipping, and Import Compliance
Clear communication prevents expensive machining errors. Send the latest drawing, 3D model, material grade, surface finish, and tolerance requirements. Mark every revision with a date and approval status. Ask the supplier to confirm unclear dimensions before production begins. A short video call can reveal details that email misses. Keep decisions in one written record. Time zones create delays.
Packaging protects precision. Specify corrosion protection for steel parts and separate finished surfaces with foam or paper. Use sealed bags, desiccant, and rigid crates for long ocean shipments. Small parts need labeled inner boxes, not loose bags. Include part numbers, quantities, and inspection status on each package. I once saw a good batch arrive with scratched surfaces because separators were too thin. The packaging plan was technically acceptable, but not practical enough.
Shipping documents require equal attention. Confirm the commercial invoice, packing list, certificate of origin, material certificates, and inspection report before dispatch. Check the HS classification with a qualified customs broker. It affects duties, declarations, and possible import controls. Verify the consignee’s legal name and delivery address carefully. Ask who handles customs clearance, insurance, and local charges under the agreed shipping terms. Import rules can change, so review destination requirements before every order. A careful checklist helps, though it cannot replace professional customs advice.
7 CNC Precision Machining Tips for Global Buyers
Use standardized drawing requirements to improve communication with suppliers, reduce packaging and shipping risks, and support import-compliance documentation.
Reference data: The chart shows ISO 2768-1 general tolerances for linear dimensions under tolerance class “m” (medium). Buyers should confirm the applicable standard, material, inspection method, packaging requirements, shipping terms, and customs documents before production.
Control Production With Inspection, Documentation, and Sample Approval
Global buyers should treat a CNC part as controlled evidence, not merely a shipment.
The 2022 ISO Survey recorded 1,265,216 valid ISO 9001 certificates worldwide.
Certification does not prove every dimension. It shows why documented control matters. Before cutting metal, freeze the drawing revision, material grade, tolerances, finish, and inspection points. Small ambiguity becomes expensive across borders.
Request a first-article inspection report for the approved sample. It should connect each characteristic with a measured value, instrument ID, calibration status, and acceptance limit. The NIST/SEMATECH e-Handbook of Statistical Methods explains that measurement uncertainty affects process decisions. A 20.000 mm reading is not automatically exact. Specify datum setup, probe method, temperature, and sampling frequency. For critical bores, request gauge repeatability evidence. Buyers often ask for photos but forget raw data. Not enough.
Use sample approval as a written production gate.
Record the sample number, drawing revision, deviations, corrective actions, and authorized signatures. Keep the same structure for in-process and final inspection records. Compare serial numbers, packing labels, and reports before dispatch.
I have seen a technically good batch delayed because its inspection report referenced an obsolete drawing. The paperwork can still fail.
No report is self-proving. Perform a small audit after the first production run, even when the sample looked perfect.
Article Source:
At Premium PSU, we are specialists in designing and manufacturing power conversion systems for the industrial market. Our product range includes high reliability power supplies from 50W to 72kW.
PREMIUM PSU
C/ Dolors Aleu, 19-21, 2nd Floor
08908 – Hospitalet de Llobregat
Barcelona-SPAIN
t.+34 93 223 26 85